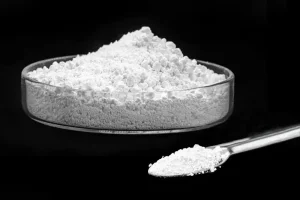
Explore our core selection of high-purity industrial and agricultural nitrate formulations designed for extreme operational environments.
Tajikistan, characterized by its mountainous topography and rapidly expanding agricultural and mining sectors, presents unique demands for industrial chemicals. The nation's drive toward modernized farming and infrastructural reinforcement requires high-grade inputs such as potassium nitrate, calcium ammonium nitrate, and specialized molten salts. As local industries scale up production capacity, sourcing dependable chemical manufacturing partners becomes paramount for sustainable economic growth.
In response to regional supply chain vulnerabilities, global procurement managers and Tajik enterprises increasingly look toward world-class Chinese manufacturing facilities. These factories offer unparalleled economies of scale, stringent quality assurance protocols, and robust logistical frameworks capable of delivering consistent chemical formulations directly to Central Asian markets.
Send Inquiry NowChinese chemical manufacturing has transitioned into an era defined by intelligent automation, strict environmental compliance, and high-purity yield optimization. Facilities specializing in the Nitrates Series leverage advanced crystallization and synthesis technologies to achieve purity levels exceeding 99.4%. For importers in Tajikistan, partnering with established Chinese producers guarantees adherence to international safety standards, customizable packaging options for arduous transport routes, and transparent lifecycle tracking.
Furthermore, robust R&D integration enables manufacturers to formulate tailor-made solutions—such as specialized anti-caking fertilizers for arid soils and high-capacity thermal storage salts for renewable energy initiatives—ensuring optimal performance across diverse climatic conditions.
Measurable metrics reflecting our industrial capacity, global reach, and technical expertise.
Why industry leaders choose our production lines for mission-critical chemical supplies.
Decades of mastery in international export operations, ensuring flawless customs clearance, regulatory compliance, and consistent product quality upon arrival.
State-of-the-art facilities yielding an annual output of 600,000 tons of molten salts and industrial nitrates, guaranteeing uninterrupted supply chains.
An expert engineering and technology support team providing rapid-response consultations for complex industrial applications and formulation adjustments.
Comprehensive selection including potassium nitrate (KNO3), sodium nitrate (NaNO3), and specialized calcium compounds to fulfill multi-industry requirements.
1. Advanced Agricultural Technology: Tajikistan's horticultural and cash crop sectors benefit immensely from water-soluble fertilizers like potassium nitrate and calcium ammonium nitrate. These compounds enhance nutrient absorption efficiency in alkaline soils, significantly increasing crop yields for cotton, orchards, and greenhouse vegetables.
2. Thermal Energy Storage Systems: As Central Asia explores renewable energy diversification, concentrated solar power (CSP) and industrial waste-heat recovery systems require high-purity nitrate molten salts as thermal energy storage media. Our products provide exceptional thermal stability across broad temperature ranges.
3. Industrial Manufacturing & Metallurgy: Utilized widely in metal heat treatment agents, glass manufacturing, and water purification agents, our nitrate series ensures precise chemical reactions and structural integrity in heavy industrial environments.
Expert answers regarding nitrate procurement, logistics, and technical specifications for international buyers.
Shipments are typically dispatched via multimodal rail and road networks connecting major Chinese manufacturing hubs through Xinjiang ports directly into logistics terminals across Tajikistan, ensuring secure and timely delivery.
Yes, we offer flexible packaging options including 25kg moisture-proof woven bags, 1000kg jumbo bulk bags, and customized palletization tailored to withstand long-distance transport and challenging storage conditions.
Our production facilities utilize advanced automated crystallization, multi-stage filtration, and rigorous laboratory spectrometry testing to guarantee every batch meets international industrial and food-grade benchmarks.
Explore our extensive range of high-performance industrial chemicals, specialized fertilizers, and water treatment agents.
 VOJIN